ASML, TSMC, and imec Demonstrate Scalable 2D Material Transistor Integration
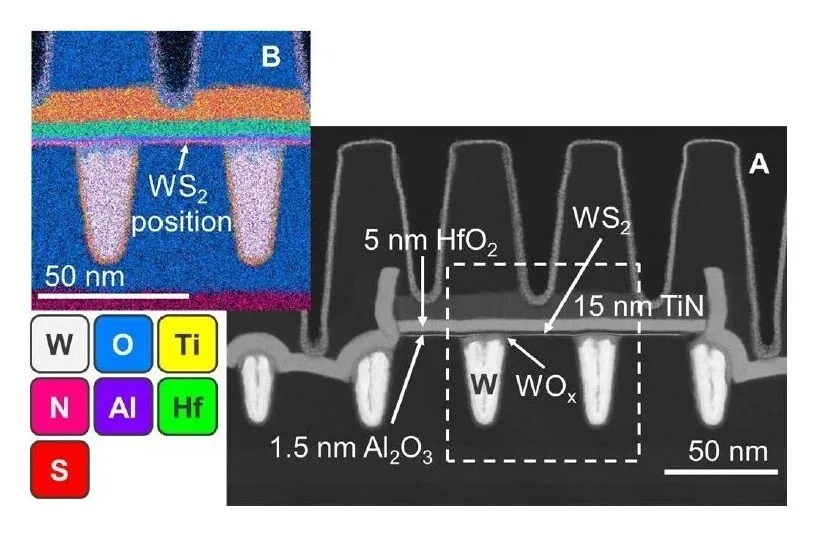
ASML, TSMC, and imec have successfully demonstrated the scalable integration of two-dimensional material transistors onto standard 300 millimeter wafers with a fifty nanometer pitch. This collaborative milestone bridges advanced research and commercial manufacturing, offering a viable pathway to extend semiconductor scaling beyond silicon limitations while maintaining industry-standard production volumes.
The semiconductor industry stands at a critical inflection point where traditional silicon scaling approaches encounter fundamental physical barriers. As transistor dimensions approach atomic thresholds, manufacturers must explore alternative materials that can maintain performance gains without triggering prohibitive power consumption or manufacturing defects. Recent developments presented at a major industry symposium highlight a coordinated effort to transition advanced transistor architectures from laboratory prototypes into standard fabrication environments. This shift represents a calculated response to the escalating demands of modern computing infrastructure.
ASML, TSMC, and imec have successfully demonstrated the scalable integration of two-dimensional material transistors onto standard 300 millimeter wafers with a fifty nanometer pitch. This collaborative milestone bridges advanced research and commercial manufacturing, offering a viable pathway to extend semiconductor scaling beyond silicon limitations while maintaining industry-standard production volumes.
What is the significance of integrating 2D materials into modern semiconductor manufacturing?
The continuous miniaturization of electronic components has driven the global technology sector for decades. Engineers have relied on silicon to deliver predictable performance improvements across successive processor generations. As feature sizes shrink, quantum tunneling effects and leakage currents begin to undermine traditional designs. Researchers have investigated two-dimensional materials as potential channel replacements because of their exceptional atomic thinness and superior electrostatic control. These materials can theoretically maintain current flow while reducing the voltage required to switch states. The successful integration of these compounds onto standard factory floors marks a decisive step toward commercial viability.
Why does the transition to 300 mm wafers matter for advanced node development?
Semiconductor fabrication relies heavily on standardized wafer dimensions to ensure economic efficiency. The thirty millimeter format has served as the industry baseline for high-volume manufacturing since the early two thousand and two era. Moving experimental transistor designs from smaller research substrates to the standard thirty millimeter diameter requires substantial engineering adjustments. Equipment calibration, chemical processing uniformity, and defect density control must all be recalibrated for larger surface areas. Achieving reliable performance on these larger platforms demonstrates that the underlying technology can support commercial production scales. This transition eliminates a major barrier that previously confined advanced materials to academic laboratories.
Understanding the 50 nm pitch milestone in transistor scaling
Pitch refers to the center-to-center distance between repeating structural elements within a transistor layout. A fifty nanometer measurement indicates a highly compressed arrangement of gates and interconnects. Maintaining this spacing while incorporating alternative channel materials demands precise lithographic alignment and advanced etching techniques. The achievement signals that the manufacturing process can handle dense patterns without compromising electrical isolation. It also suggests that existing factory infrastructure can potentially accommodate these new architectures with minimal redesign. This level of precision is essential for sustaining performance trajectories in next-generation processors.
How do ASML, TSMC, and imec collaborate to bridge research and production?
The semiconductor supply chain operates through tightly coupled partnerships between equipment makers, research institutes, and fabrication facilities. imec functions as a central innovation hub that develops foundational technologies and validates manufacturing pathways. ASML supplies the extreme ultraviolet lithography systems required to print increasingly complex circuit patterns. TSMC operates the advanced foundry operations that translate validated designs into reliable commercial products. This triad represents a complete ecosystem capable of moving innovations from theoretical models to mass production. Their joint presentation at the 2026 IEEE/JSAP Symposium on VLSI Technology and Circuits underscores a unified strategy to overcome scaling bottlenecks.
The physical limits of silicon and the search for alternative channel materials
Silicon has served as the foundational semiconductor material for over half a century. Its crystalline structure and oxide properties have enabled decades of predictable scaling. However, atomic-scale dimensions introduce fundamental constraints that no amount of process refinement can fully resolve. Leakage currents increase exponentially as channel lengths decrease, leading to unacceptable power waste. Two-dimensional materials offer a different physical profile that can suppress these unwanted currents. Their layered atomic structure allows for tighter control over electron movement. The industry recognizes that continuing to rely solely on silicon will eventually stall performance improvements.
What are the manufacturing challenges associated with 2D-material integration?
Translating laboratory successes into factory-ready processes requires overcoming numerous engineering hurdles. Material transfer techniques must preserve atomic integrity while ensuring uniform coverage across large surfaces. Chemical compatibility between the new channel layers and existing gate stacks demands rigorous testing. Thermal processing steps must not degrade the delicate two-dimensional structures during standard fabrication sequences. Defect density must remain exceptionally low to prevent yield losses in high-volume production. Each manufacturing step introduces variables that can compromise electrical performance. The demonstrated robustness indicates that these variables have been successfully managed through iterative process development.
Implications for future computing architectures and power efficiency
The successful validation of this architecture carries broad implications for the technology sector. Reduced operating voltages directly translate to lower thermal output and extended battery life for mobile devices. Data centers can achieve higher computational density without requiring proportional increases in cooling infrastructure. The ability to maintain performance gains while controlling power consumption addresses a critical constraint facing modern computing. Manufacturers can continue to deliver faster processors without triggering unsustainable energy demands. This progression supports the continued expansion of artificial intelligence workloads and high-performance computing applications.
What does this milestone mean for the future of semiconductor scaling?
The industry has consistently navigated scaling challenges through collaborative innovation and incremental process improvements. This particular achievement demonstrates that alternative materials can meet the stringent requirements of commercial fabrication. It provides a concrete pathway for extending transistor density beyond traditional silicon boundaries. The demonstrated scalability suggests that foundries can adopt these architectures without completely overhauling existing production lines. Researchers can now focus on optimizing interface properties and refining patterning techniques for subsequent generations. The foundation has been established for the next phase of architectural evolution.
Long-term industry trajectories and technological adoption
Semiconductor development follows a predictable cycle of research, validation, and commercial deployment. The current milestone accelerates the timeline for widespread adoption of advanced channel materials. Equipment manufacturers will adjust lithography and deposition tools to support these new requirements. Design teams will begin developing standardized cell libraries optimized for the new transistor characteristics. The broader technology ecosystem will benefit from sustained performance improvements and improved energy efficiency. This coordinated effort ensures that the industry remains on a sustainable growth trajectory.
How does extreme ultraviolet lithography enable such precise patterning?
Printing features at the fifty nanometer pitch requires sophisticated optical systems capable of resolving incredibly fine details. Extreme ultraviolet lithography utilizes specialized mirrors and plasma sources to generate wavelengths short enough to expose advanced photoresists. The integration of two-dimensional materials demands that these optical systems maintain exceptional focus across the entire wafer surface. Any deviation in alignment can compromise the electrical characteristics of the final transistors. The successful demonstration confirms that current lithography platforms can support next-generation material architectures without fundamental redesigns.
What economic factors drive the adoption of standardized fabrication platforms?
High-volume manufacturing depends on strict standardization to minimize capital expenditure and maximize output. The thirty millimeter wafer format allows foundries to amortize equipment costs across millions of chips. Transitioning experimental designs to this standard platform ensures that future production runs remain economically viable. Smaller research wafers cannot support the throughput required by global supply chains. Achieving reliable results on the standard format proves that the technology can compete with existing silicon processes in both performance and cost efficiency.
How are material transfer techniques adapted for industrial environments?
Transferring atomically thin layers from growth substrates to target wafers requires precise mechanical and chemical handling. Industrial environments demand processes that can operate continuously without introducing particulate contamination. Advanced transfer mechanisms utilize controlled pressure differentials and specialized carrier layers to preserve structural integrity. These techniques must be compatible with existing cleanroom protocols to avoid disrupting normal operations. The successful demonstration indicates that these transfer methods have been refined to meet the rigorous standards of commercial fabrication.
What role does yield optimization play in commercial deployment?
Yield optimization remains a critical factor in transitioning advanced technologies from prototype to production. Foundries monitor defect rates across every processing step to identify potential bottlenecks. The integration of new channel materials introduces additional variables that must be tightly controlled. Statistical process control methods help manufacturers maintain consistent electrical performance across entire wafer lots. The reported robustness suggests that yield management strategies have been effectively implemented. This level of control is essential for achieving the profitability required to sustain long-term manufacturing operations.
Future research directions and architectural evolution
Continued refinement of these architectures will require sustained investment in materials science and process engineering. Researchers will focus on improving interface quality and reducing parasitic resistance within the new transistor structures. Advanced simulation tools will help design teams predict performance characteristics before physical prototyping begins. The industry will also explore complementary approaches that combine traditional silicon with novel channel materials. These parallel development paths will ensure that computing infrastructure continues to meet growing global demands.
The semiconductor sector continues to navigate a complex landscape of physical constraints and escalating computational demands. The collaborative demonstration of scalable two-dimensional material integration onto standard manufacturing platforms represents a decisive advancement. By addressing critical engineering challenges and validating commercial viability, the participating organizations have cleared a major hurdle. The industry now faces the task of refining these processes and preparing for subsequent architectural iterations. Sustained progress depends on continued cooperation between research institutions and production facilities. The path forward remains grounded in methodical engineering and shared technological objectives.
What's Your Reaction?
 Like
0
 Dislike
0
 Love
0
 Funny
0
 Wow
0
 Sad
0
 Angry
0
Christopher Holloway is the founder and director of Progressive Robot, a UK-based technology company. A full-stack engineer with more than two decades of experience, he works across PHP development, ecommerce, Linux infrastructure, technical SEO and AI automation, and writes here on technology, AI, hardware and software.


Comments (0)